OEM CNC Machined 6061 Aluminum Alloy in China
Custom CNC machining of 6061 aluminum alloy components for OEM customers worldwide — from a single machined prototype to repeat high-volume production runs. As a China-based precision machining workshop, we turn 6061 bar, plate, block and tube into brackets, shafts, flanges, housings, heat sinks and structural parts that go straight into our customers' assemblies.
Our floor combines CNC turning centers, three-axis vertical machining centers, four-axis rotary machining and simultaneous five-axis milling, supported by drilling, tapping and a complete set of secondary finishing operations. Every CNC machined 6061 aluminum part produced in our China workshop is programmed from the customer's native 3D model, fixtured to control deformation, and checked feature by feature against the drawing before it leaves the floor.
Buyers looking for CNC machined 6061 aluminum in China usually care about the same four things: dimensional consistency, clean cosmetic surfaces, predictable delivery, and engineering communication that genuinely understands a drawing. This page explains the material we machine every day, how 6061 is named under standards around the world, which processes we run in-house, and how an order moves from a STEP file to a fully inspected, packed component.
Typical 6061 Aluminum Components on Our Floor
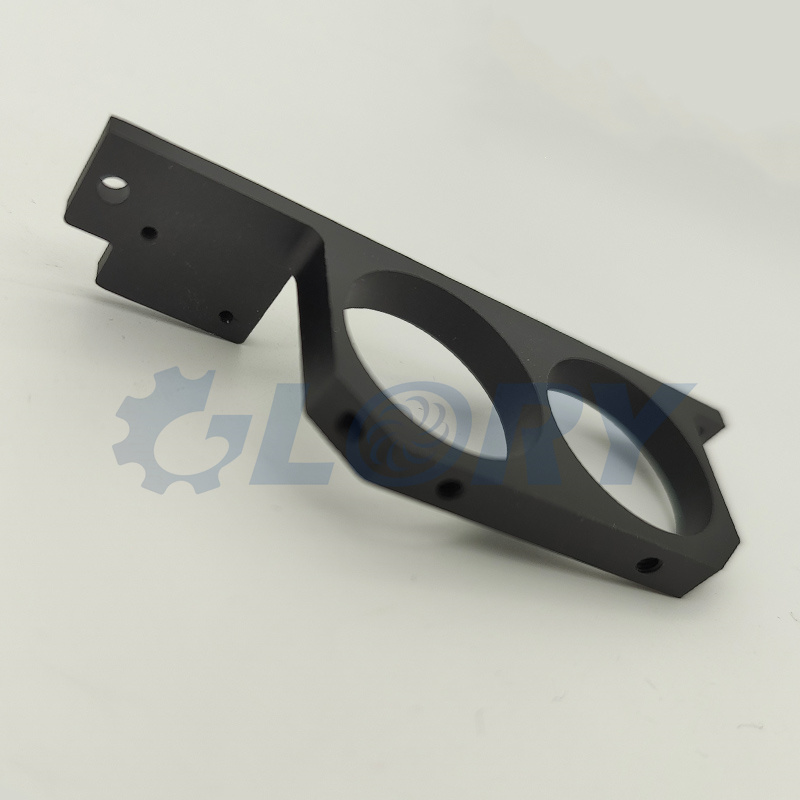
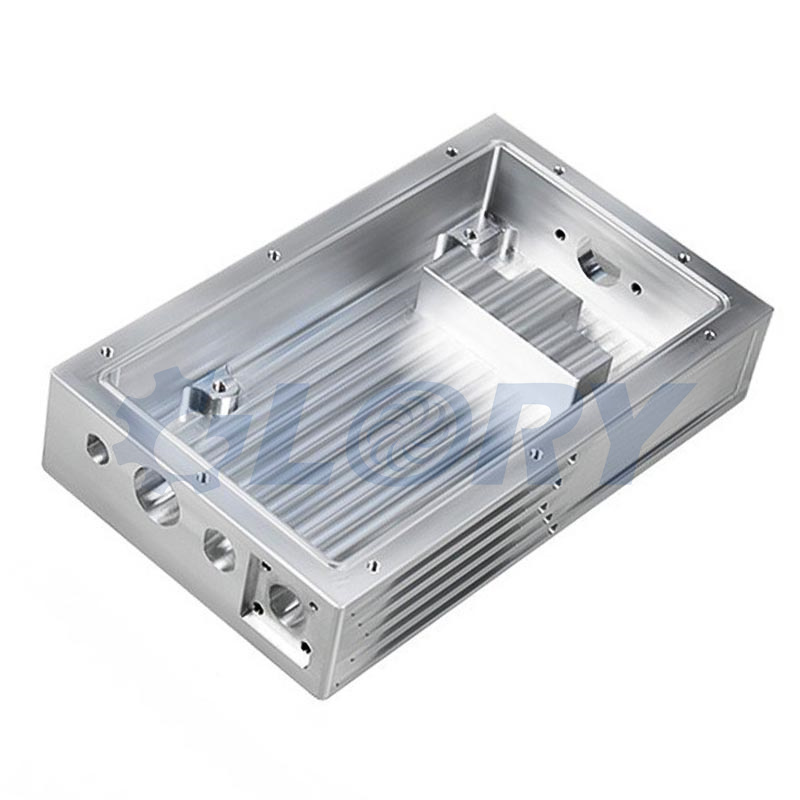
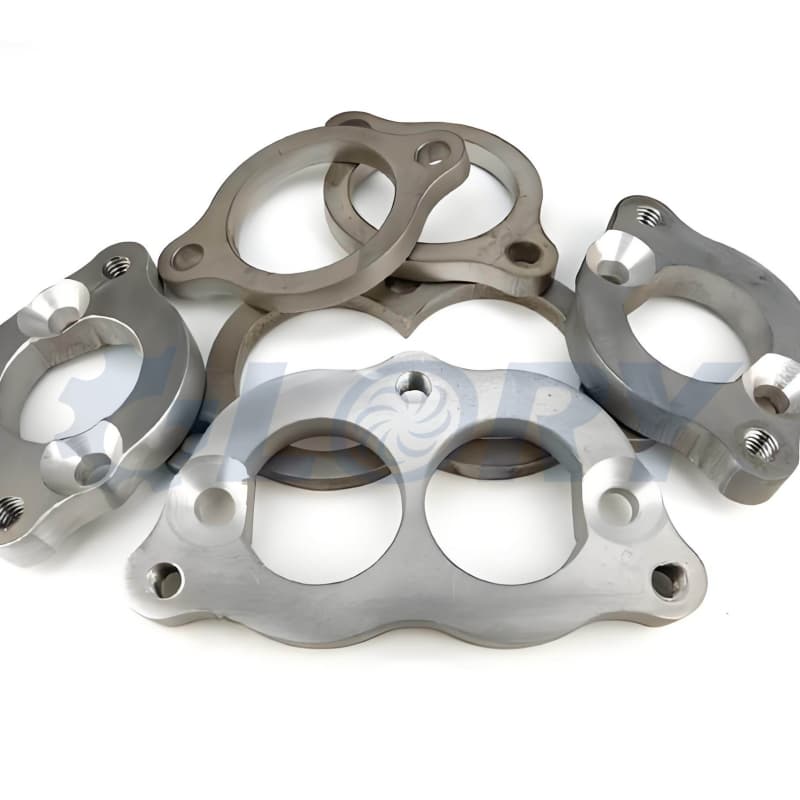
A small selection of parts machined from 6061 aluminum. Each component is made to the customer's own drawing rather than stocked as a standard catalog item, which is the normal way CNC machined 6061 aluminum in China is supplied to OEM buyers.

What 6061 Aluminum Alloy Is
6061 is a wrought, heat-treatable aluminum alloy in the 6xxx series, where magnesium and silicon are the principal alloying elements. During solution heat treatment and artificial aging, these elements combine into extremely fine Mg₂Si precipitates distributed through the aluminum matrix. It is this precipitation structure that gives 6061 its useful balance of mechanical strength, toughness and corrosion resistance, without making the material difficult or abrasive to machine.
Because of that balance, 6061 has become one of the most frequently requested alloys whenever customers source CNC machined 6061 aluminum in China. It machines cleanly at high spindle speeds, welds well, accepts anodizing evenly, and remains dimensionally stable after material is removed — properties that matter equally for a one-off robot flange and for a repeating batch of ten thousand mounting brackets.
The alloy is commercially available as extruded round bar, square and flat bar, plate, sheet, tube and custom extruded profiles, and it is supplied in several tempers. Most machined structural parts are ordered in T6 or T651 condition, while the soft O temper is selected when bending or forming has to take place before any final aging step.
6061 Material Profile at a Glance
- Alloy series6xxx series, aluminum – magnesium – silicon system
- Principal elementsmagnesium and silicon, with controlled copper content
- Strengthening methodMg₂Si precipitation hardening after heat treatment
- Tempers for machiningT6, T651 and T6511 are the most common
- Density2.70 g/cm³, roughly one third the density of steel
- Stock forms we useround bar, plate, block, square bar, flat bar and seamless tube
- Typical machined partsbrackets, plates, housings, shafts, flanges, heat sinks, jigs and fixtures
- Machining behaviorshort chips, high achievable feeds, good surface finish with sharp tooling
How 6061 Is Named Under Different Material Standards
The same 6061 chemistry carries different designations in different national and regional material standards. The table below helps match drawings, purchase specifications and incoming stock when a project references a non-US designation. These are material designation systems — they describe the alloy itself, not any approval of a supplier.
| Region / Material System | Standard Family | Equivalent Designation | Notes for Machined Parts |
|---|---|---|---|
| North America – Aluminum Association | AA / ANSI H35.1 | AA 6061 | The reference registration used on most international drawings |
| United States – Unified Numbering System | UNS | UNS A96061 | Common in American aerospace-style and industrial specifications |
| Europe | EN 573 | EN AW-6061 | European wrought aluminum designation, chemistry defined in EN 573-3 |
| International | ISO 209 | AlMg1SiCu | ISO chemical composition naming based on element content |
| Germany | DIN | 3.3214 / AlMg1SiCu | Numeric material number alongside the symbolic name |
| Japan | JIS H4000 / H4040 | A6061 | Frequently seen on Japanese machinery and robotics drawings |
| China | GB/T 3190 | 6061 | The standard designation used for domestic Chinese stock and export parts |
| Russia | GOST 4784 | AD33 (АД33) | Historical equivalent occasionally seen on legacy drawings |
| United Kingdom | BS | 6061 (formerly BS H20) | Older British designation replaced by the European EN system |
On Chinese stock and export paperwork, the GB designation 6061 represents the same chemistry as AA 6061, so a CNC machined 6061 aluminum part made in China can be produced against a drawing that calls out EN AW-6061, JIS A6061 or UNS A96061 without changing the underlying material. We cross-check the called-out standard against the actual stock chemistry before cutting begins.
Chemistry and Mechanical Behavior of 6061
The figures below explain why 6061 machines and behaves the way it does. Values are typical published ranges for the alloy and for the T6 temper; exact numbers vary slightly with product form, section thickness and temper.
Chemical Composition (weight %, max or range)
| Silicon (Si) | 0.40 – 0.80 |
| Iron (Fe) | 0.70 max |
| Copper (Cu) | 0.15 – 0.40 |
| Manganese (Mn) | 0.15 max |
| Magnesium (Mg) | 0.80 – 1.20 |
| Chromium (Cr) | 0.04 – 0.35 |
| Zinc (Zn) | 0.25 max |
| Titanium (Ti) | 0.15 max |
| Other elements, each | 0.05 max |
| Aluminum (Al) | Balance |
Typical Physical & Mechanical Values, 6061-T6
| Ultimate tensile strength | ≥ 310 MPa (about 45 ksi) |
| Yield strength | ≥ 276 MPa (about 40 ksi) |
| Elongation at break | approximately 10 – 17 % by thickness |
| Shear strength | approximately 207 MPa |
| Fatigue strength | approximately 96 MPa (5×10⁸ cycles) |
| Modulus of elasticity | 68.9 GPa |
| Brinell hardness | approximately 95 HB |
| Density | 2.70 g/cm³ |
| Melting range | 582 – 652 °C |
| Thermal conductivity | approximately 167 W/(m·K) |
| Coefficient of thermal expansion | 23.6 µm/(m·°C), 20 – 100 °C |
| Electrical conductivity | approximately 43 % IACS |
6061 Tempers Explained for Designers
Choosing the correct temper before machining controls both strength and how much a part moves after material is removed. These four conditions cover nearly every CNC machined 6061 aluminum component produced in our China workshop.
O — Annealed
Fully soft and highly formable. Used when bending, deep forming or spinning must happen first, with strength added by a later heat treatment. Rarely machined as a final-state structural temper.
T4 — Naturally Aged
Solution heat-treated and then aged naturally at room temperature. Offers moderate strength and is sometimes specified where limited forming follows heat treatment.
T6 — Artificially Aged
Solution heat-treated followed by controlled artificial aging. This is the standard high-strength temper for most turned and milled 6061 components and offers the best all-round machinability.
T651 / T6511 — Stress Relieved
Aged and then mechanically stretched to remove residual internal stress. Preferred for thick plates and tight-tolerance parts because components distort far less after heavy machining.
Why Designers Choose Machined 6061 Aluminum
Six properties explain why 6061 appears in everything from robot structures to electronic enclosures, and why it remains the default alloy for most buyers searching for CNC machined 6061 aluminum in China.
Strength Without Excess Weight
In T6 condition the alloy reaches roughly 310 MPa tensile strength at only 2.70 g/cm³. That strength-to-weight ratio supports brackets, frames, mounting plates and robot links while keeping moving assemblies light and reducing inertia.
Atmospheric Corrosion Resistance
A natural protective oxide film forms on the surface, giving good resistance to normal atmosphere, fresh water and many industrial environments. Anodizing thickens and seals this layer for outdoor or cosmetic applications.
Predictable, Fast Machinability
6061 forms short, manageable chips and allows high spindle speeds and feeds with sharp tooling and flood coolant. Tool life is stable, built-up edge is rare, and fine finishes are achievable without slow, expensive finishing cycles.
Welding and Joining Flexibility
The alloy welds well by TIG and MIG and can also be brazed or assembled with helical inserts and press-fit hardware. Designers should note that strength close to a weld is locally reduced, so load paths are planned accordingly.
Versatile Surface Finishing
6061 accepts clear or color anodizing, hard-coat anodizing, bead blasting, brushing, polishing, powder coating and laser marking with even, repeatable results — a major reason it is chosen for visible enclosure and panel parts.
Useful Thermal and Electrical Behavior
With thermal conductivity around 167 W/(m·K) and electrical conductivity near 43 % IACS, machined 6061 works well for heat sinks, cooling plates, conduction paths and shielded electronic housings.
In-House CNC Machining Processes for 6061
Turning, milling across three, four and five axes, drilling and tapping are combined on one floor, so a 6061 part can move from raw stock to a finished component without repeated outside handling.
CNC Turning
CNC lathes and turning centers, including machines with live tooling, handle outer- and inner-diameter turning, facing, grooving, parting and thread cutting. Typical 6061 work includes shafts, sleeves, spacers, standoffs, bushings, threaded fittings and piston-style parts, with close attention to concentricity, cylindricity and turned surface roughness.
3-Axis CNC Milling
Vertical machining centers produce faces, steps, shoulders, pockets, slots, contours and regular drilled and tapped hole patterns from a single working direction. Three-axis milling is the fastest, most economical route for prismatic plates, brackets and simple housings, and it handles the majority of everyday CNC machined 6061 aluminum work in our China shop.
4-Axis CNC Milling
A fourth rotary axis indexes or rotates the component so that multiple sides, radial holes and cross-features can be machined in one setup. This removes the alignment error that comes from repeatedly re-clamping a part and is well suited to elongated profiles, manifold-style bodies and parts with features on several faces.
5-Axis CNC Milling
Both 3+2 positional and full simultaneous five-axis machining reach compound angles and continuously curved surfaces. Impellers, curved robot flanges, contoured housings and parts with angled hole patterns are completed in fewer setups, with shorter tools, improved rigidity and a more uniform surface finish.
CNC Drilling
Controlled drilling sequences — center spotting, piloting, peck drilling, reaming and boring — protect hole position and straightness, including deeper holes in 6061 plate and block. Coolant-fed drilling and staged peck cycles clear chips reliably and prevent work hardening around the hole wall.
CNC Tapping
Internal threads are cut or formed in metric coarse and fine sizes as well as unified UNC/UNF series. Roll-form taps are used for suitable blind holes in aluminum to gain stronger, cleaner threads, while helical interpolation is used for larger thread sizes and for fragile thin-wall sections where a solid tap would risk distortion.
From One Single Piece to Large-Batch Production
There is no fixed minimum order quantity. The same programming and inspection discipline is applied to a single prototype and to a repeating production lot, so a design can scale without changing supplier. The quantity bands below are illustrative and are always confirmed per part.
Single Piece & Prototype
One-off and very small runs for fit checks and design verification. We review the model for manufacturability, select an efficient setup, machine the part and run a complete first-article inspection before anything is shipped.
Pilot & Low Volume
Pilot batches support field testing and early assembly. Fixtures and tool paths are refined across the first runs, cycle times settle, and the production process is locked in before quantities grow.
Mid-Volume Series
Repeat batches use multi-vise setups, soft jaws, tombstone fixtures and optimized roughing and finishing strategies to drive down the unit price while keeping feature consistency from the first piece to the last.
High-Volume Production
Large, scheduled production runs rely on repeatable fixturing, planned tool life, in-process patrol checks and standardized compartment packaging, so repeated orders of CNC machined 6061 aluminum from our China workshop arrive identical batch after batch.
How a 6061 Machining Order Moves Through the Workshop
A transparent six-step path keeps quality built into the process rather than added at the end, which matters for both a single CNC machined 6061 aluminum part made in China and a continuous production program.
Drawing and Model Review
The 3D model (STEP, IGES or Parasolid) is compared against the 2D PDF drawing to catch tolerance stack-ups, impossibly thin walls, un-millable internal corners and ambiguous thread or surface callouts before any steel is cut.
Material Planning
Bar, plate or tube is selected in the correct temper, with grain direction considered for plate parts and adequate oversizes left for facing and squaring. Stock origin and batch records are kept with the job.
Programming and Fixturing
CAM tool paths are planned around clamping deformation, using soft jaws, vacuum plates, custom fixtures or tombstones so that thin 6061 sections stay supported through roughing and finishing.
CNC Machining
Roughing brings the part close to net shape, a stabilizing pause or staged material removal lets stress relax on thin parts, and light finishing passes then hold flatness, parallelism and final surface quality.
Inspection
First-article, in-process and outgoing checks use calibrated hand tools, thread and pin gauges, a 2D profile projector and a 3D coordinate measuring machine to verify the features called out on the drawing.
Finishing and Packing
Deburring, edge breaking, blasting, anodizing or other finishes are applied, parts are cleaned and dried, and cosmetic surfaces are individually bagged and compartment-packed to survive international shipping.
Workshop, Machining and Inspection
Where CNC machined 6061 aluminum in China is actually produced and verified — the equipment floor and the measurement steps that stand behind every outgoing batch.
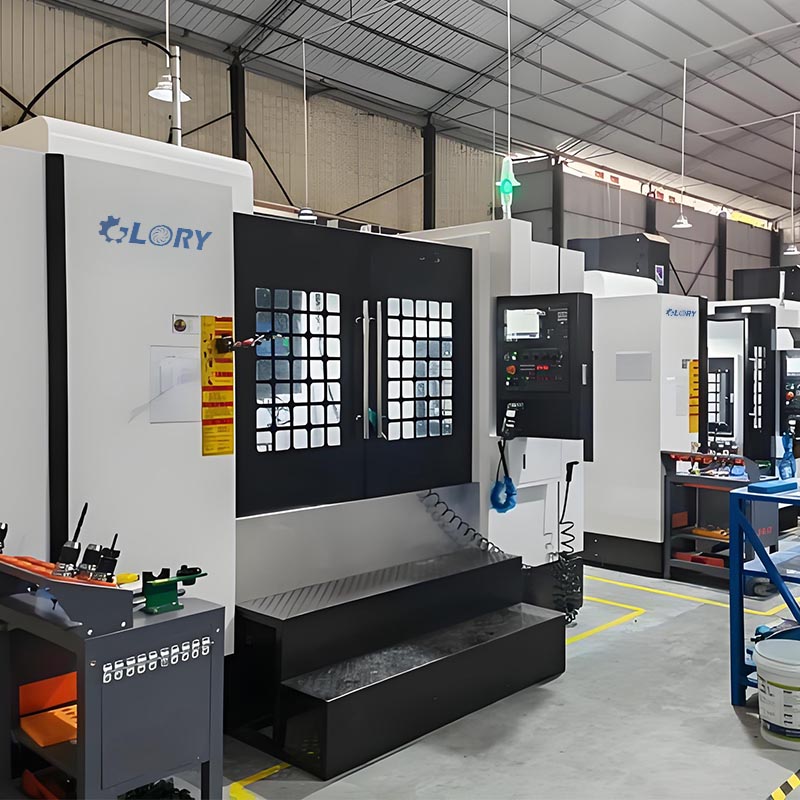
Workshop
An organized CNC floor with separate turning and milling cells, structured tooling storage and a dedicated inspection area that keeps measurement away from cutting vibration and coolant mist.
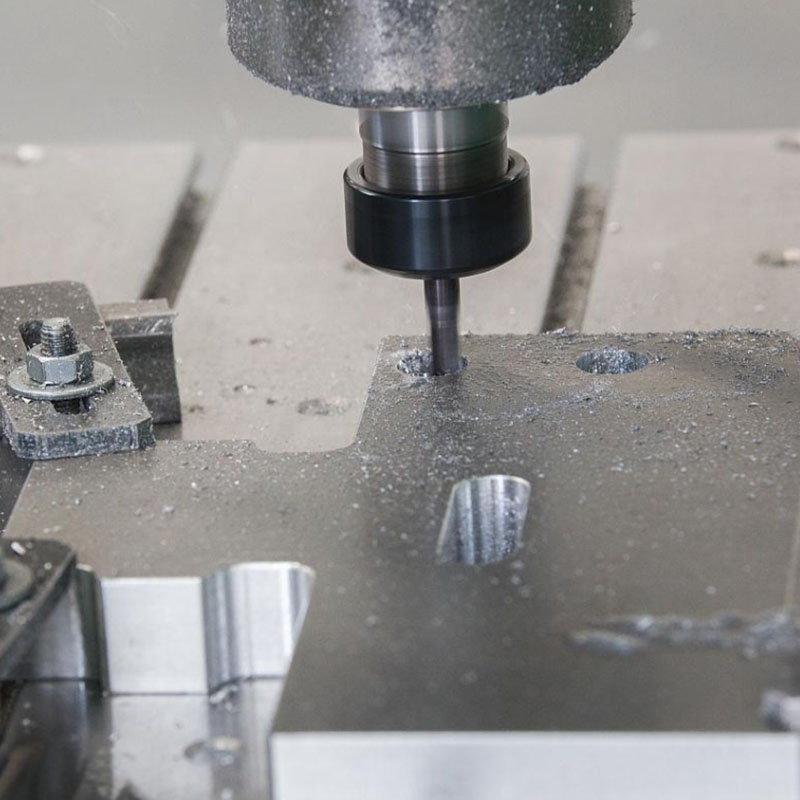
CNC Milling
Vertical machining centers combine face milling, pocketing, contouring, drilling and tapping on 6061 plates and blocks within a single setup, preserving position accuracy across the whole hole pattern.
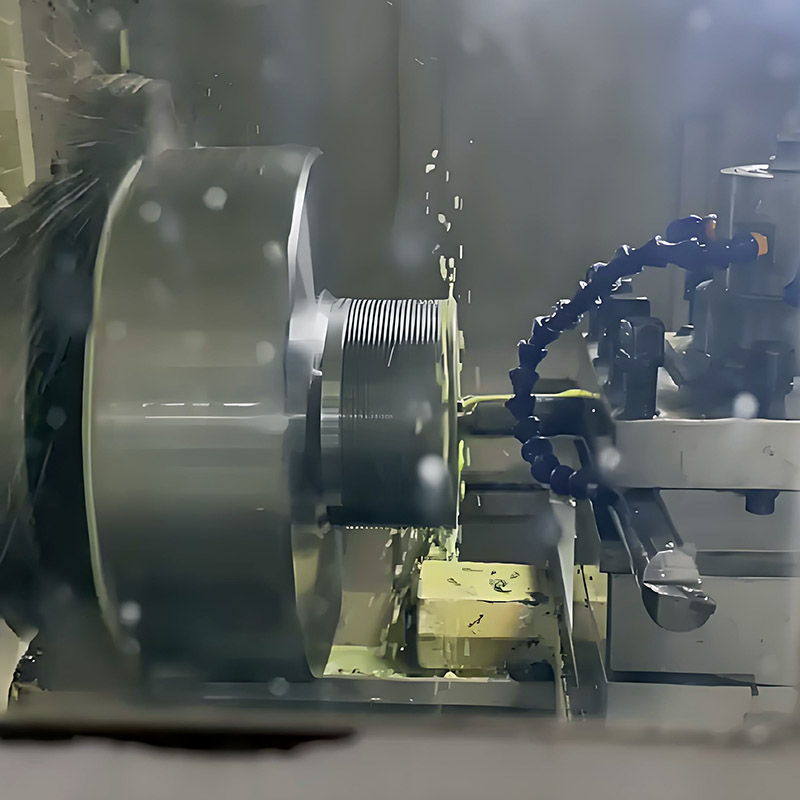
CNC Turning
Turning centers produce rotational 6061 components such as motor shafts, sleeves, standoffs, spacers and threaded fittings, with live tooling adding cross-holes and milled flats without a second machine.
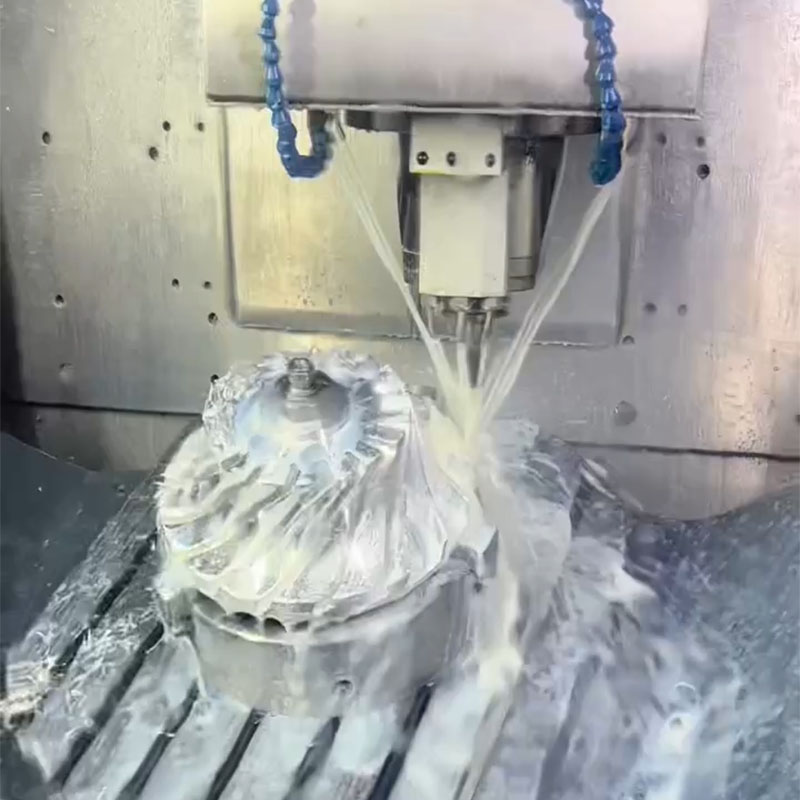
5-Axis Milling
Simultaneous five-axis machining handles continuously contoured surfaces, impeller blades, compound-angle holes and complex robot and automation components in fewer, more rigid setups.
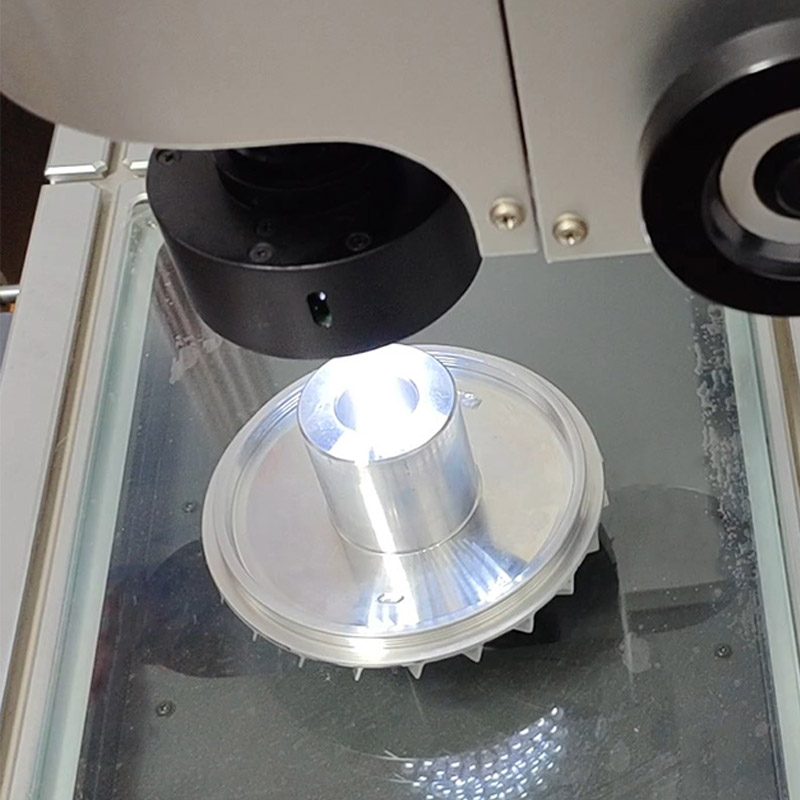
2D Measuring
A profile projector magnifies 2D section profiles to verify radii, chamfers, angles, blade contours and edge geometry that are difficult to judge reliably with hand tools alone.
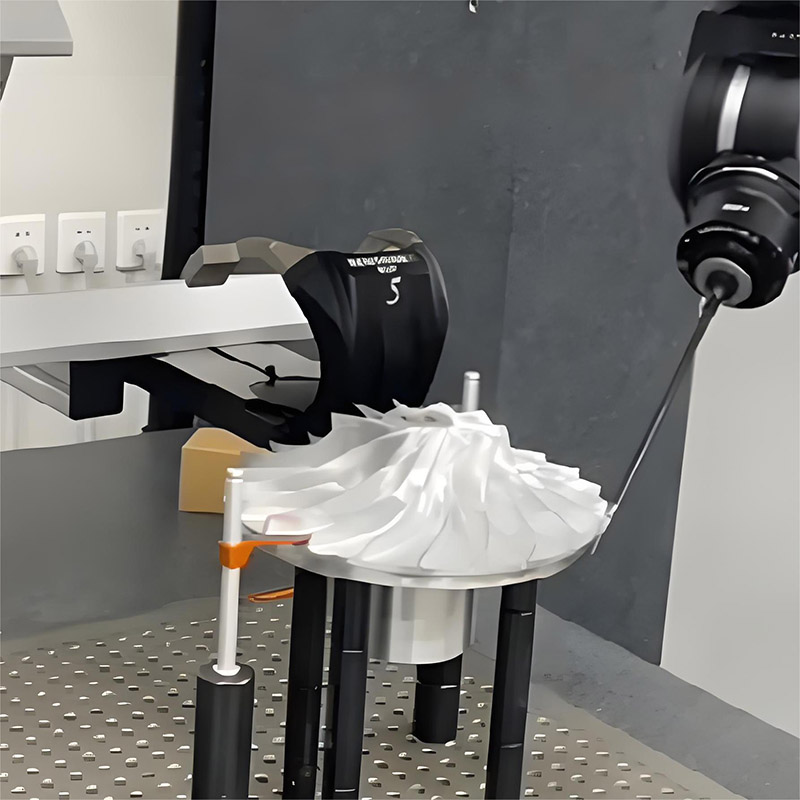
3D Measuring
A coordinate measuring machine captures three-dimensional point data to confirm true position, flatness, profile of a surface and the spatial relationship between features on complex 6061 parts.
Industries That Use Our 6061 Components
The same 6061 alloy serves very different engineering environments. These eight sectors account for most of the CNC machined 6061 aluminum components produced in our China workshop.
Robotics & Automation
Robot arm links, connecting flanges, sensor brackets, gripper jaws and motion-system plates where low inertia and precise hole patterns are essential.
Automotive & Electric Vehicles
Mounting brackets, adapter plates, busbar supports, cooling plates and prototype drivetrain components that benefit from light weight and thermal conduction.
Electronics & Telecommunications
Shielded enclosures, chassis panels, front panels, heat spreaders and rack components that require clean cosmetic finishes and accurate cut-outs.
Industrial Machinery
Machine plates, fixture blocks, guide mounts, sensor holders and replacement mechanism parts for production lines and specialized equipment.
Marine & Outdoor Equipment
Deck fittings, mounting rails, camera housings and outdoor structural parts that rely on the natural corrosion resistance of 6061, often enhanced by anodizing.
Renewable Energy Systems
Tracking-system brackets, inverter mounting plates, cooling bodies and structural connectors for solar, wind and energy storage installations.
Medical & Laboratory Equipment
Equipment frames, instrument housings, tray supports and adjustment mechanisms for non-implant devices where clean machining and controlled finishes matter.
UAVs & Ground Support Equipment
Lightweight airframe structures, camera gimbals, docking hardware and ground-support tooling where every gram saved improves payload and endurance.
Secondary Operations and Surface Finishes
Machining is only half of a finished component. These six finishing paths are coordinated alongside production so a CNC machined 6061 aluminum part from China arrives ready to assemble, with no loose burrs or unfinished edges.
Deburring and Edge Breaking
Manual and mechanical deburring removes machining burrs, breaks sharp edges to controlled radii or chamfers, and cleans cross-holes and internal slots where chips can become trapped.
Bead Blasting and Satin Texture
Fine glass-bead blasting produces a uniform matte satin surface that hides tool marks and handling lines, creating an ideal base for consistent anodizing on visible parts.
Clear and Color Anodizing
Clear, black or colored anodizing adds a controlled oxide layer for wear and corrosion protection, with repeatable shades used for identification or product branding.
Brushing, Polishing and Tumbling
Directional brushing, mechanical polishing and vibratory tumbling deliver cosmetic effects ranging from industrial linear grain to bright, smooth decorative surfaces.
Powder Coating and Wet Painting
Durable colored coatings protect parts used outdoors or in customer-facing equipment, with masking used to keep critical mating faces and threaded holes coating-free.
Laser Marking and Labeling
Permanent part numbers, revision letters, orientation marks and serial identifiers are laser-etched onto machined surfaces without introducing stress or raised material.
Dimensional Control on Machined 6061 Parts
Tolerances always follow the customer drawing. Where a drawing invokes a general medium-grade workshop practice for non-critical dimensions — for example the ISO 2768 medium class — that rule is applied consistently to every un-toleranced feature. On explicitly controlled dimensions, machined 6061 features are routinely held in the plus-or-minus 0.01 mm class when the design, stock and setup support it, and tighter requirements are reviewed feature by feature during the drawing review.
Surface roughness is controlled through tool selection, feed planning and finishing passes: turned and milled 6061 surfaces commonly reach Ra 1.6 µm or smoother on critical faces. Flatness and parallelism on thin plates are protected by choosing stress-relieved T651 stock, roughing symmetrically, leaving a uniform finishing allowance and taking light skim passes from both sides in sequence.
Inspection Routine Behind Every Batch
- Incoming stock checkalloy, temper, dimensions and batch record verified before machining
- First-article checkfull feature inspection on the first completed component
- In-process patrolkey dimensions re-checked as the batch progresses and tools wear
- Outgoing checkfeatures re-confirmed against the drawing before packing
- Hand measuring toolscalipers, micrometers, bore and height gauges, dial indicators
- Thread and hole gaugesring and plug thread gauges, pin gauges and feeler gauges
- 2D and 3D equipmentprofile projector and coordinate measuring machine for complex geometry
- Batch recordsmeasurement notes retained with the order for repeat production
Practical Questions About Machined 6061
Questions that come up repeatedly when engineers and procurement teams plan an order for CNC machined 6061 aluminum in China.
Which temper should appear on my drawing?
T6 is the safe default for general machined parts. Specify T651 or T6511 for thick plates and tight-tolerance components that must not move after machining, and O only when forming must happen before a later heat treatment.
Can you work from a 3D model only?
A 3D model is enough to program the geometry, but a 2D PDF drawing is strongly preferred because it carries thread specs, tolerances, surface requirements and notes that do not live inside a solid model. STEP, IGES and Parasolid files are all accepted.
Is there a minimum order quantity?
No. A single prototype piece is accepted, and the price per piece naturally decreases as quantity rises because setup and programming effort is spread across a larger batch.
How are thin 6061 walls kept from deforming?
Stress-relieved stock, symmetric roughing, a reserved finishing allowance, soft-jaw or vacuum support and very light finishing passes distribute cutting forces evenly and stop thin walls from springing or vibrating.
Which thread standards can be produced?
Metric coarse and fine threads, unified UNC and UNF threads, and selected parallel pipe threads can be tapped, thread-formed or helically interpolated, with thread gauges used to confirm fit before parts leave the floor.
Why source CNC machined 6061 aluminum in China?
A mature local 6061 supply chain, fast access to bar and plate in every temper, dense anodizing and finishing capacity, and competitive machining cost combine to support both fast prototypes and steady batch production in one location.
A Practical Partner for CNC Machined 6061 Aluminum in China
Sourcing CNC machined 6061 aluminum in China works best when the workshop understands the material as well as the machine. We select the correct temper, cross-reference AA, EN, JIS, GB and UNS designations against the drawing, plan fixtures around the deformation behavior of aluminum, and combine turning, three-, four- and five-axis milling, drilling and tapping under one roof so that geometry, threads and cosmetic surfaces all come from a single controlled process.
That approach scales with the product: a single prototype receives the same drawing review and first-article inspection as a five-figure production lot, and repeat orders reuse the proven program, fixturing and inspection notes so later batches match the first. The result is a straightforward supply path for OEM teams that need dependable 6061 components without managing a chain of separate process vendors.
From material selection and international grade cross-reference to five-axis machining and CMM-verified dimensions, every step is built around one outcome: a CNC machined 6061 aluminum component in China that matches the drawing, the assembly and the production schedule.
About Us
 We provide custom machined parts, 5-axis linkage CNC machining, and the design, production, and assembly of machinery and equipment.
