OEM CNC Machined 316 Stainless Steel in China
We are a China-based CNC machining workshop focused on corrosion-resistant alloys, and we produce OEM CNC machined 316 stainless steel in China for customers who need dependable parts for wet, chemically active, and hygienic operating environments. Every component is manufactured from the customer’s own drawings, STEP/IGES models, and samples — there is no fixed catalog, because every order is built to your dimensions, tolerances, thread forms, and surface requirements. This page explains the material itself, the different national-standard grade names that appear on international drawings, the machining processes we run in-house, the full range of order quantities we support, and the way finished parts are measured before shipment.
In-House CNC Machining Processes for 316 Stainless Steel
The processes below are all available under one roof, so a typical order of CNC machined 316 stainless steel in China can move from a saw-cut bar to a finished, inspected part without relying on outside process steps. Process selection follows the geometry: rotational features go to the lathe, prismatic and contoured features go to the milling centers, and hole-making and threading are planned around how 316 work-hardens during cutting.
CNC Turning
Bar-fed and chucked CNC lathes produce rotational 316 parts such as adapters, bushings, spacers, nipples, ferrules, and pump shafts. Operations cover OD/ID turning, facing, boring, grooving, parting, knurling, and single- or multi-start external and internal thread cutting. Live-tool lathes add cross-holes, flats, and milled features in a single clamping, preserving concentricity between turned and secondary features.
3-Axis CNC Milling
Vertical machining centers cut prismatic 316 components — mounting flanges, brackets, manifold blocks, and valve bodies — along X, Y, and Z. This route handles pockets, steps, slots, planar faces, drilled and tapped hole patterns, and 2.5D profiles with repeatable positioning from the first piece to the last piece of the batch.
4-Axis CNC Milling
A rotary fourth axis indexes or continuously rotates the workpiece so several faces of a 316 part are machined in one setup. It is used for cross-drilled fittings, radial bolt circles, helical grooves, and parts where face-to-face squareness is critical, removing the alignment drift that repeated manual re-fixturing introduces.
5-Axis CNC Milling
Simultaneous five-axis machining reaches complex 3D surfaces, angled holes, and undercuts on 316 workpieces — impellers, curved housings, and multi-port fluid components. Shorter, stiffer tools can reach deep cavities because the spindle or table tilts toward the feature, improving surface finish and feature-to-feature accuracy while collapsing multiple setups into one.
Drilling, Reaming & Boring
Precision hole-making covers straight holes, cross holes, stepped holes, relatively deep holes, counterboring, countersinking, spot-facing, and reamed or bored holes for close IT-grade fits. Peck cycles and through-coolant drills manage chip evacuation in 316, where a rubbed, work-hardened hole wall is the most common cause of drifting diameters and tight bores.
Tapping & Thread Milling
Internal threads are produced by tapping or helical thread milling in metric, unified, and pipe forms — M, UNC/UNF, BSPP/G, and NPT where the part geometry allows. Thread milling is preferred for expensive 316 components and for fine or large threads: pitch diameter can be tuned to the required class of fit, and a worn cutter can never be broken off inside a nearly finished part.
How 316 behaves on the machine — and how the process is built around it
316 is not difficult to cut, but it punishes dull tools and hesitation. Its austenitic structure work-hardens under a rubbing edge, and its chips are long and stringy with a tendency toward built-up edge. The practical response is sharp inserts with polished chipbreakers and positive-rake geometry, rigid work-holding, a continuously engaged cut without dwelling, generous flood coolant at the cutting zone, and speeds and feeds calibrated to the insert grade rather than to carbon-steel habits. Bores are split into roughing and finishing passes, and thin-walled 316 parts use light, balanced stock removal so that clamping and cutting stresses do not release as distortion after unclamping.
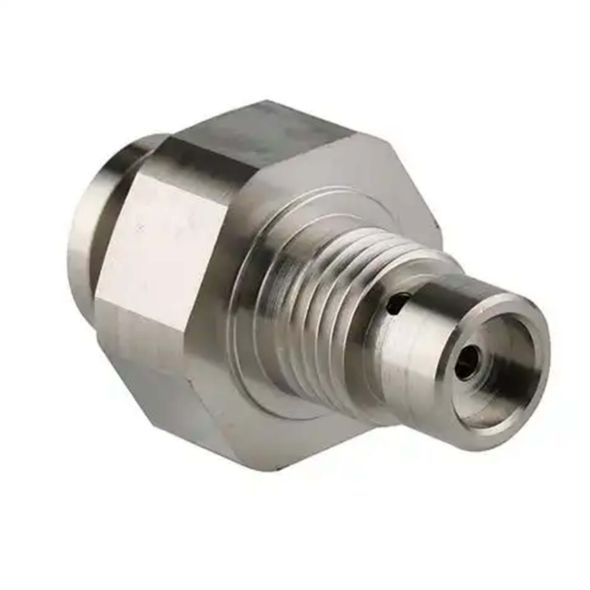
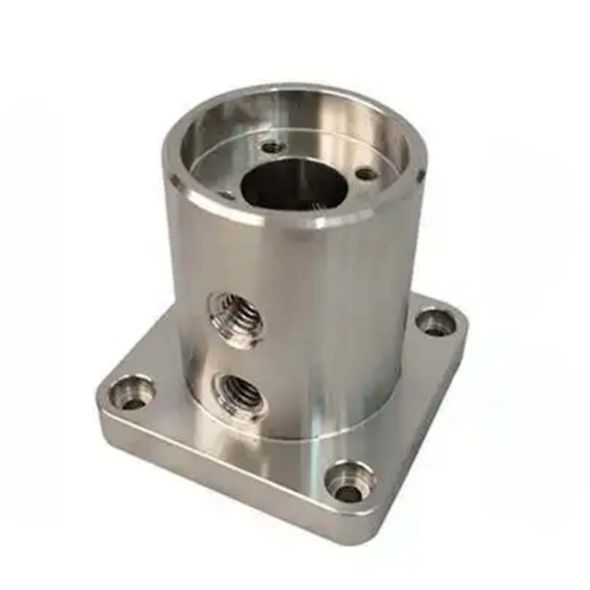
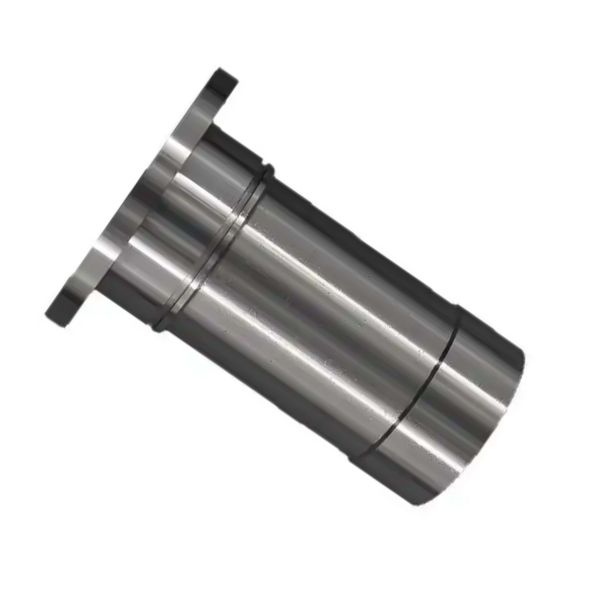
Sample CNC Machined 316 Stainless Steel Components
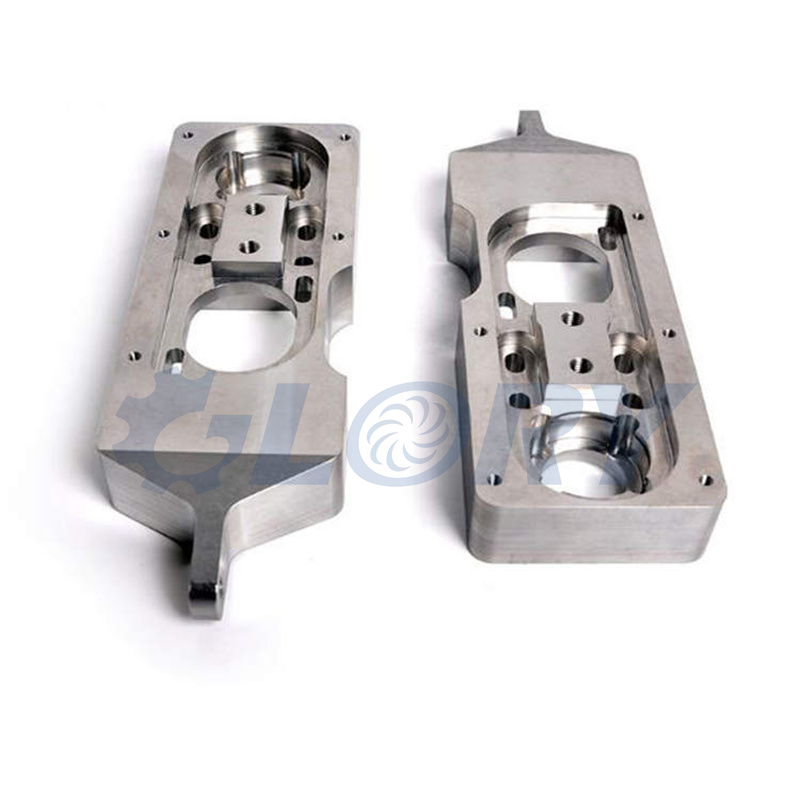
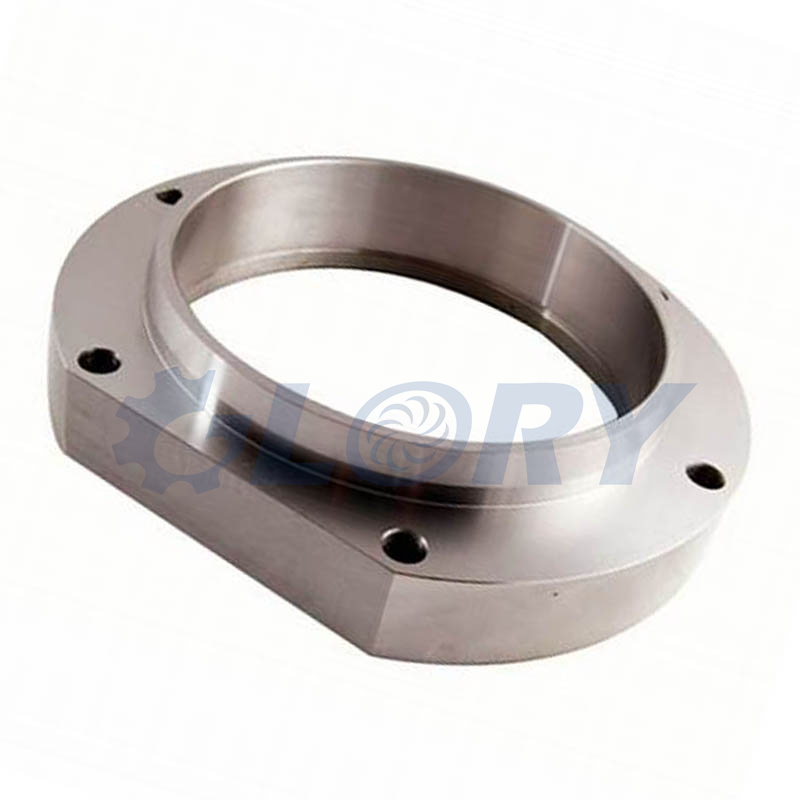
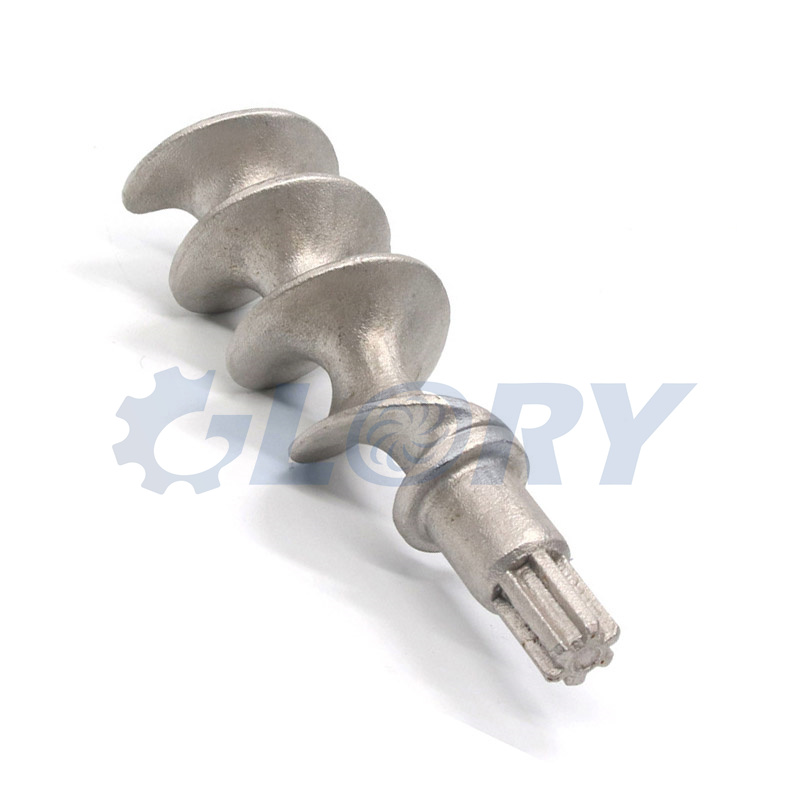
A selection of recurring part families among CNC machined 316 stainless steel in China orders — adapters, mounting flanges, precision bushings, machined components, retaining rings, and screw shafts for food machinery, all produced to customer drawings.
316 Stainless Steel Grade Cross-Reference by National Standard
Drawings from different countries rarely use the same name for the same alloy. AISI 316 is an American designation; the same molybdenum-bearing austenitic chemistry appears under EN, DIN, BS, JIS, GB/T, and GOST numbers. When CNC machined 316 stainless steel in China is produced against an overseas drawing, the incoming bar, plate, or forging is normally supplied to the Chinese GB/T designation, which maps directly to the grade printed on your drawing.
| Standard system / region | Equivalent of 316 (standard carbon) | Equivalent of 316L (low carbon) | Typical product standards |
|---|---|---|---|
| USA — AISI / ASTM / UNS | 316 · UNS S31600 | 316L · UNS S31603 | ASTM A276 bar, A182 F316 forgings, A240 plate/sheet, A312 TP316 pipe |
| Europe — EN 10088 | 1.4401 / X5CrNiMo17-12-2 | 1.4404 / X2CrNiMo17-12-2 | EN 10088-3 bar, EN 10088-2 sheet/plate, EN 10222-5 forgings |
| Germany — DIN / WN | 1.4401 / X5CrNiMo17-12-2 | 1.4404 / X2CrNiMo17-12-2 | DIN 17440 bar, DIN 17441 sheet/strip |
| United Kingdom — BS (BS 970) | 316S31 / 316S16 | 316S11 / 316S12 | BS 970-1 bar, BS 1449 sheet/strip |
| Japan — JIS | SUS316 | SUS316L | JIS G4303 bar, JIS G4305 sheet/plate |
| China — GB/T 20878 | 06Cr17Ni12Mo2 (formerly 0Cr17Ni12Mo2) | 022Cr17Ni12Mo2 (formerly 00Cr17Ni12Mo2) | GB/T 1220 bar, GB/T 4237 plate, GB/T 14976 fluid pipe |
| Russia — GOST (analogue) | 08Kh17N13M2 | 03Kh17N14M3 | GOST 5632 alloy grades (near-equivalent chemistries) |
Note: 316 and 316L share the same corrosion-alloy family and differ mainly in maximum carbon content; 316Ti variants (EN 1.4571 / SUS316Ti / 06Cr17Ni12Mo2Ti) use titanium stabilization instead of extra-low carbon and are selected mainly for welded high-temperature service.
| Chemical composition (wt %, annealed product) | ||
|---|---|---|
| Element | 316 / S31600 | 316L / S31603 |
| Carbon, C | ≤ 0.080 | ≤ 0.030 |
| Manganese, Mn | ≤ 2.00 | ≤ 2.00 |
| Silicon, Si | ≤ 0.75 | ≤ 0.75 |
| Phosphorus, P | ≤ 0.045 | ≤ 0.045 |
| Sulfur, S | ≤ 0.030 | ≤ 0.030 (lower-sulfur heats on request) |
| Chromium, Cr | 16.00–18.00 | 16.00–18.00 |
| Nickel, Ni | 10.00–14.00 | 10.00–14.00 |
| Molybdenum, Mo | 2.00–3.00 | 2.00–3.00 |
| Nitrogen, N | ≤ 0.10 | ≤ 0.10 |
| Iron, Fe | Balance | Balance |
Composition limits per ASTM A240 / A276; product-form standards may carry minor differences.
| Physical & mechanical properties (annealed) | |
|---|---|
| Property | Typical value |
| Density | ≈ 7.98 g/cm³ |
| Melting range | 1,375–1,400 °C |
| Thermal conductivity at 100 °C | ≈ 16.3 W/(m·K) |
| Mean thermal expansion, 0–100 °C | ≈ 16.0 µm/(m·K) |
| Electrical resistivity at 20 °C | ≈ 7.4 × 10⁻⁷ Ω·m |
| Elastic modulus | ≈ 193 GPa |
| Tensile strength Rm, min. | ≥ 515 MPa |
| 0.2% proof strength Rp0.2, min. | ≥ 205 MPa |
| Elongation A (50 mm), min. | ≥ 40% |
| Hardness, max. | 217 HB / 95 HRB |
| Structure / magnetism | Austenitic; essentially non-magnetic when annealed |
Values are typical for annealed flat and bar product; exact minima vary slightly with product form and section size.
Material Characteristics That Drive Design Decisions
The points below explain why engineers move from 304 to 316, when the low-carbon 316L version is specified instead, and which properties matter once the drawing reaches the machine shop.
Chloride corrosion resistance from molybdenum
The 2.0–3.0% molybdenum addition is what separates 316 from 304. It sharply improves resistance to pitting and crevice attack in chloride-bearing water, salt spray, sweat, and many process chemicals. Its pitting resistance equivalent number, PREN = Cr + 3.3Mo + 16N, typically sits near 24, making it the standard choice for marine fittings, coastal equipment, and parts that see repeated wet-and-dry cycles.
Performance across temperature
Annealed 316 retains useful strength and oxidation resistance at elevated temperature and stays tough at cryogenic temperatures. The low-carbon 316L variant resists sensitization — chromium-carbide precipitation in weld heat-affected zones — so welded assemblies and parts intended for prolonged service in the 425–815 °C range are generally drawn in 316L.
Forming, welding, and cleanability
316 draws, bends, spins, and welds readily with matching 316/316L filler metal, and it takes fine machining, brushing, mirror polishing, electropolishing, and passivation finishes. Its smooth, non-porous surface survives repeated CIP/SIP cleaning and sterilization cycles, which is why it is widespread in food, dairy, beverage, pharmaceutical, and medical contact components.
Non-magnetic austenitic structure
In the annealed state 316 is essentially non-magnetic, with relative permeability close to 1, which matters for sensors, instruments, and electronic housings. Heavy cold work can induce a weak magnetic response; when non-magnetic behavior is a functional requirement, it should be stated on the drawing so stress relief or a higher-nickel chemistry can be planned in advance.
From One Single Part to High-Volume Production
Order quantity never changes the grade, but it changes fixturing, cycle strategy, and inspection sampling. CNC machined 316 stainless steel in China covers the entire quantity spectrum, and the ranges below indicate how a typical order is approached as volume grows.
Single part & first article
One-off 316 components for prototypes, fit checks, engineering samples, and replacement parts for older machines. There is no minimum order — a single cut length of bar is enough. A first-article dimensional record can accompany the part before any series is released.
Small-batch production
Roughly 1–500 pieces for design validation, field trials, and spare-part stocks. Soft jaws and simple dedicated fixtures keep setup cost low while the drawing and process are being frozen, and design revisions between batches remain inexpensive to absorb.
Repeated serial production
Roughly 500–5,000 pieces per release. Dedicated fixtures, optimized CAM toolpaths, and fixed tooling lists stabilize cycle time and unit cost. Heat-number records and inspection results are kept run by run so repeat orders match earlier deliveries.
High-volume series
Quantities of 5,000 pieces and above run on bar-fed lathes and fixtured milling centers, with planned tool-life management, scheduled in-process checks, and statistical sampling — so the 5,000th component comes off the machine matching the first one measured.
Quantity bands are indicative; the practical breakpoint for each part depends on its size, cycle time, and fixture design.
Tolerances, Finishes, and Other Machining Details
These are the details most often clarified during drawing review. Where a requirement is not stated, general workshop practice applies and is confirmed before cutting begins.
Dimensional tolerances
General tolerances follow ISO 2768-mK unless the drawing states otherwise. Bores, shaft diameters, and hole positions routinely hold ±0.01–0.02 mm on machined features, while closer requirements use fine boring, reaming, or a grinding/honing path planned at quotation stage.
Surface roughness
As-machined 316 surfaces typically reach Ra 1.6–3.2 µm; fine turning and finish boring reach Ra 0.8 µm on sealing surfaces. Brushing, bead blasting, mirror polishing, and electropolishing are available where function, cleaning, or appearance demands them.
Threads & fit systems
Metric, unified, and pipe threads are cut to the class of fit shown on the drawing, and clearance or interference fits such as H7/g6 are selected by application. Chamfers and thread undercuts are planned so burrs do not form at thread runout or at cross-holes.
Deburring & traceability
Every part is deburred and cleaned of cutting fluid, swarf, and loose chips before inspection. Incoming heat numbers, raw-material dimensions, and inspection records are filed against each order, so a repeat order two years later can be matched to the same material source and process.
Industries Served with CNC Machined 316 Stainless Steel Parts
The applications below share one requirement: a component that keeps its dimensions and its surface integrity while working in moisture, process chemicals, washdown cycles, or salt-laden air.
Marine & coastal equipment
Rigging hardware, antenna and sensor mounts, deck fittings, shaft components, and pump parts exposed to salt spray and splash, environments where 304 would begin to show pitting after relatively short service.
Food, beverage & dairy machinery
Screw shafts, valve bodies, sanitary adapters, filler nozzles, mounting brackets, and conveyor components that survive daily washdown, cleaning agents, and repeated steam or hot-water cycles.
Medical & laboratory instruments
Instrument bodies, fluid-contact fittings, housings, and precision mechanism parts, most often produced from 316L for its extra-low carbon, clean polished surface, and compatibility with sterilization routines.
Chemical & process equipment
Metering components, manifold blocks, probe holders, spray components, and small welded assemblies handling acids, brines, alkaline solutions, and process fluids at moderate temperatures.
Fluid handling, pumps & valves
Adapters, couplings, bushings, mounting flanges, ferrules, retaining rings, and threaded fittings for pumps, valves, filters, and pipe systems across both metric and inch dimensional standards.
Instrumentation & electronics
Essentially non-magnetic sensor housings, connector bodies, mounting plates, and precision enclosures where dimensional stability, corrosion resistance, and weak magnetic permeability all matter at the same time.
Machining, Workshop, and Inspection Capabilities
Production and measurement are kept as separate, sequential steps: parts come off the machine, move through deburring and cleaning, and then reach 2D and 3D inspection against the drawing before packaging.
Workshop
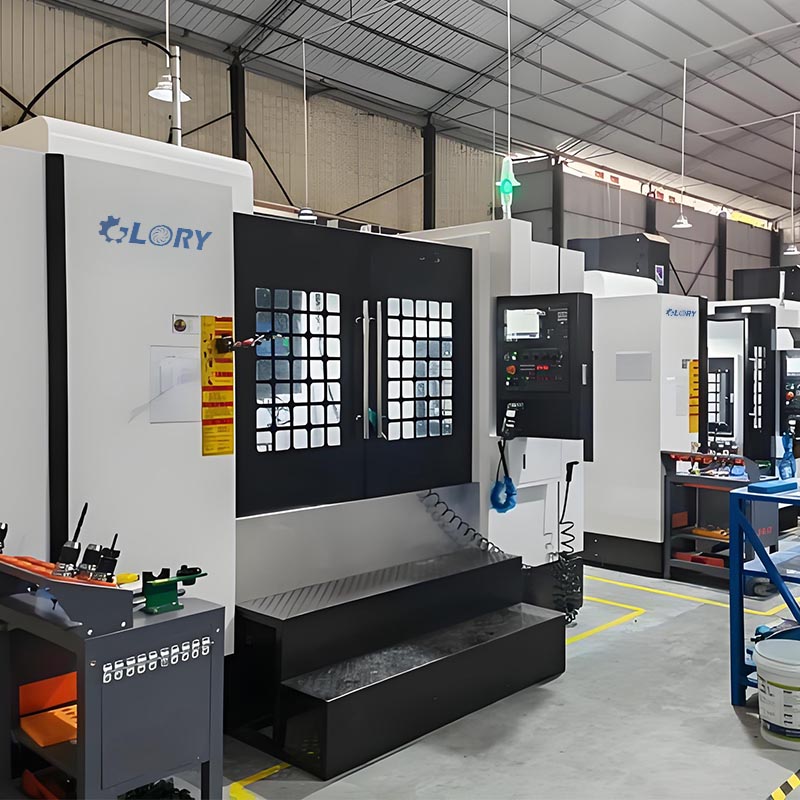
The floor layout separates turning, milling, sawing, and inspection areas, so material flow from raw bar to finished-part measurement stays orderly and traceable.
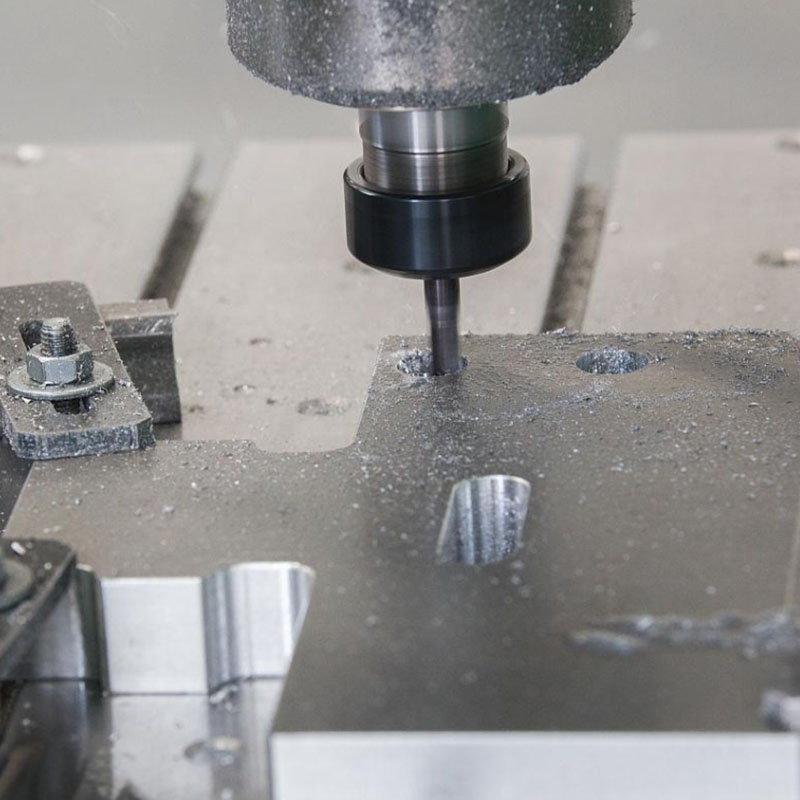
CNC Milling
Vertical machining centers handle 3- and 4-axis work on prismatic 316 parts, with flood coolant, programmed peck cycles, and fixturing sized to the order quantity.
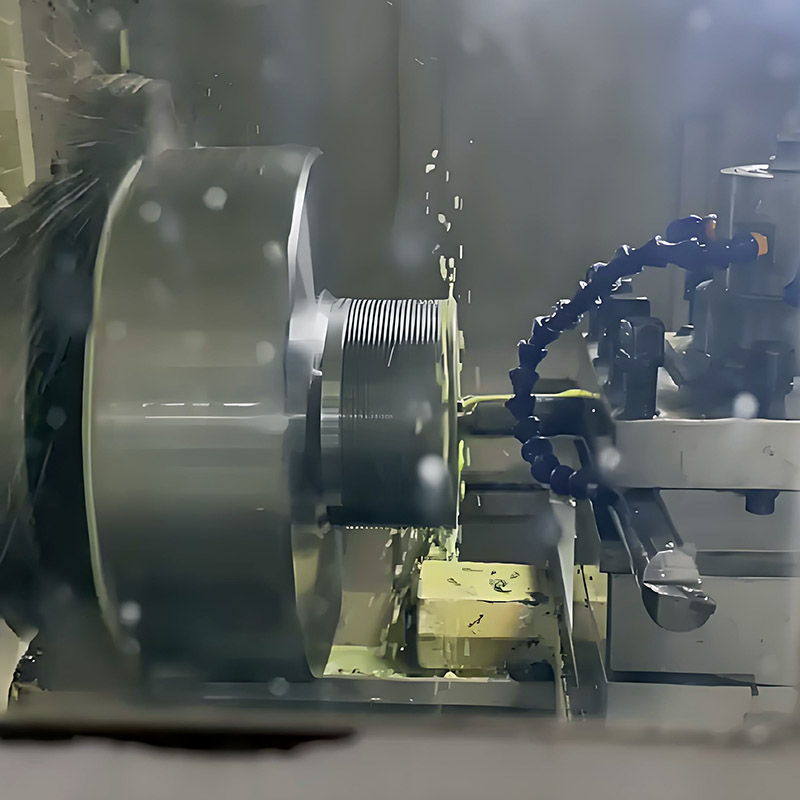
CNC Turning
CNC lathes with bar feeders produce rotational 316 components from short bushings and fittings to long threaded screw shafts, with live tooling for cross-holes and milled flats.
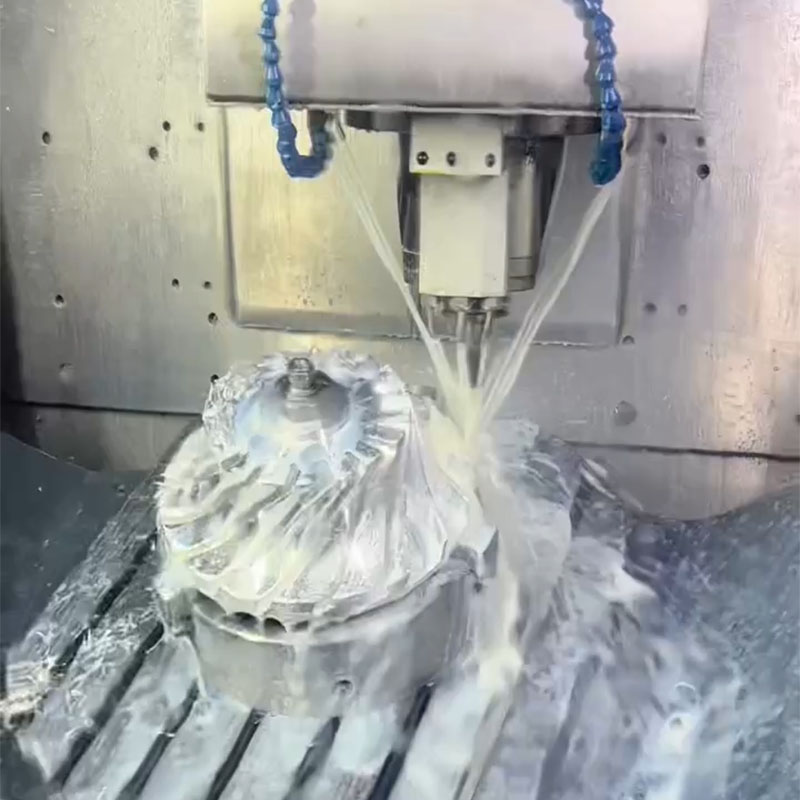
5-Axis Milling
Five-axis platforms machine contoured and multi-angle 316 workpieces in fewer setups, using shorter, stiffer tooling to protect both surface finish and feature-to-feature accuracy.
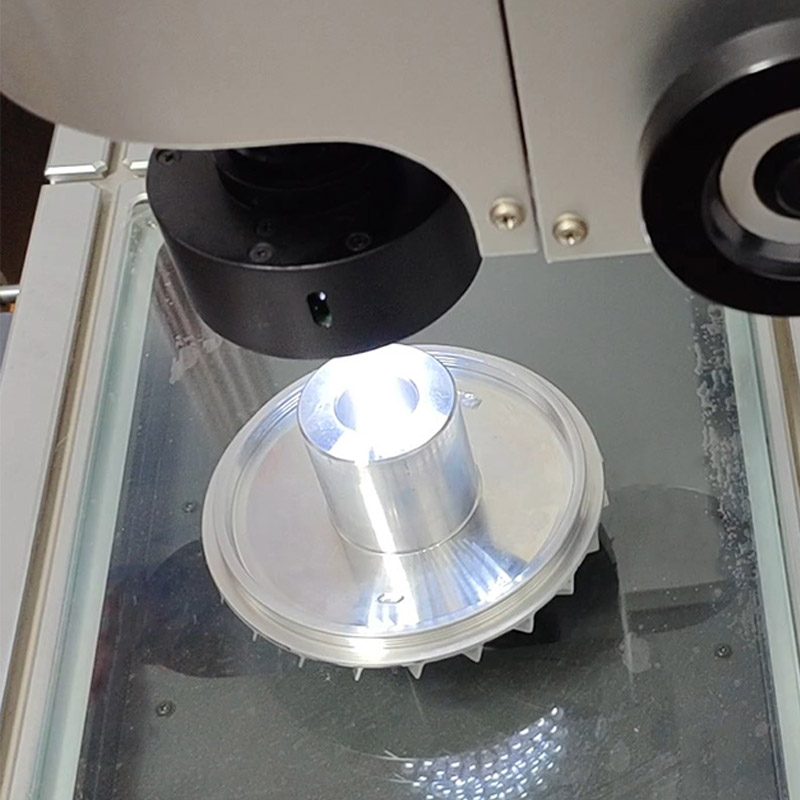
2D Measuring
A digital profile projector and vision measurement station check 2D profiles, radii, angles, thread forms, chamfers, and small-feature dimensions directly against the drawing.
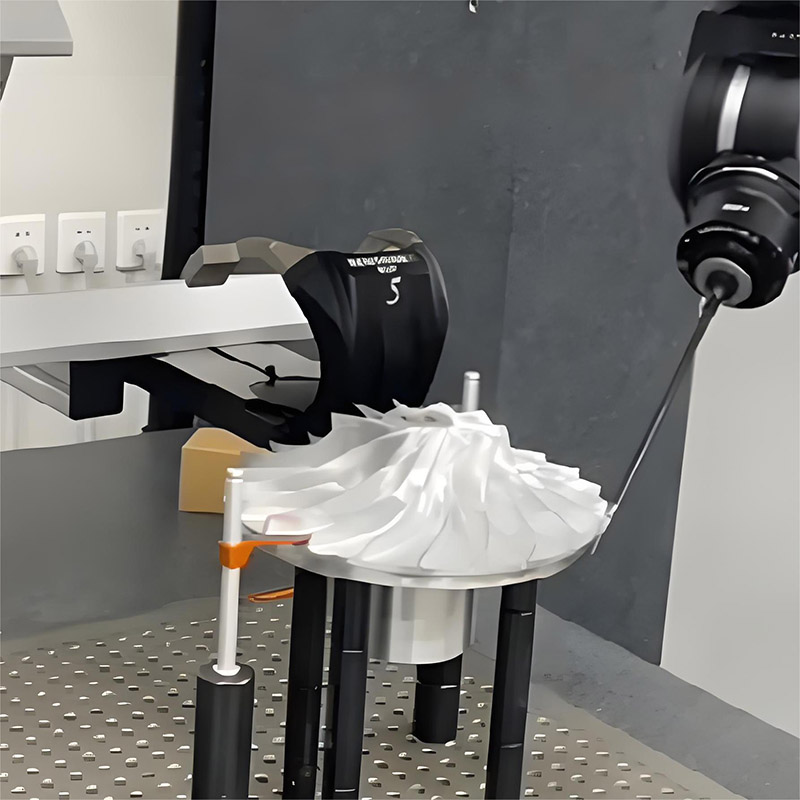
3D Measuring
A coordinate measuring machine verifies 3D geometry — true position, flatness, concentricity, profile, and complex surfaces — for first articles and batch sampling.
Sourcing CNC Machined 316 Stainless Steel in China
Sourcing CNC machined 316 stainless steel in China means matching three things at once: the correct grade chemistry for the service environment, a cutting process built around 316’s work-hardening behavior, and measurement discipline that survives repeat orders year after year. From a single replacement bushing to a recurring series of flanges, fittings, and screw shafts, every order is built to the customer’s drawing, measured against that same drawing, and shipped ready for assembly. Whether the drawing calls the material 316, SUS316, 1.4401, or 06Cr17Ni12Mo2, the machining plan starts from the same molybdenum-bearing austenitic stainless steel — and the same controlled process route.
About Us
 We provide custom machined parts, 5-axis linkage CNC machining, and the design, production, and assembly of machinery and equipment.
